Warehouse Labor Tracking: Why the Shift Plan and the Actual Headcount at Each Process Differ
2026-09-17
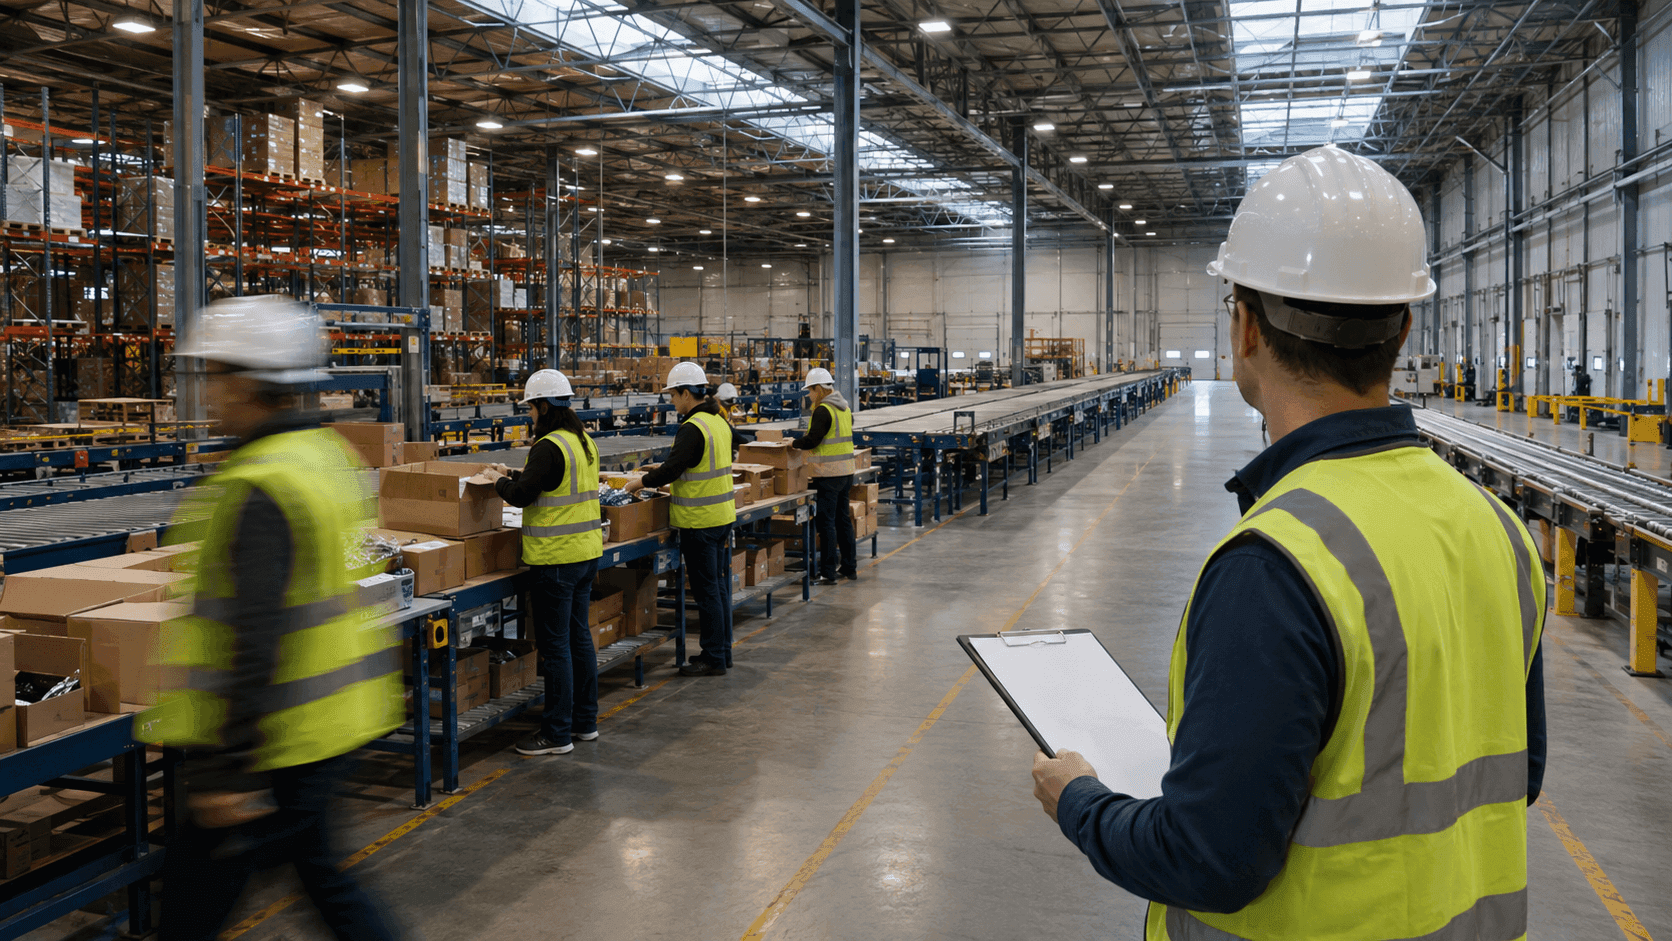
Warehouse labor tracking usually starts with a scene like this one. At 3 p.m., the shift plan lists 12 people in the inspection zone. The supervisor looks down the aisle at that zone and sees seven. The other five are over in packing, or standing in front of outbound freight waiting for a forklift, or have not come back from picking yet. Which one it is, you only find out by walking over and asking. An afternoon where the number on the plan and the number on the floor do not match is not unusual in a logistics center. It happens every day.
The problem is not that the gap exists. Volume swings from hour to hour, and people move with it. The problem is that nobody records the gap. When the day ends, only the plan survives, and where people actually were survives only in the supervisor's memory. Next week's roster is built on top of that memory.
This article is about matching warehouse labor allocation to RTLS location data. Not clock-in records, but how long each person spent at which process during working hours, how to count that distribution, and how to feed it back into the roster.
I. The plan is written in the morning and the floor changes in the afternoon
The shift plan is made the evening before or the morning of. Expected volume, the number of people on shift and break times go in, and people are divided up by process. Up to this point, every logistics center looks about the same.
But from the moment the plan is finished, the floor starts drifting away from it. Inbound that was expected in the morning slips to the afternoon, the packing line empties out because of a shipment that failed inspection, and which process the extra hands were sent to is known only to the person who sent them. The plan is the day's intent; the actual distribution is the day's result. Of course they differ.
What turns an ordinary difference into a problem is that the difference disappears. By evening the result is gone and only the intent remains on paper. So the next plan becomes a slightly edited copy of the last one, and the same waiting repeats at the same process.
Doesn't the team lead already know from walking the floor?
People who know the floor say this: one lap by the team lead and you know where it is crowded and where it is empty. That is true. But one person walking once is one scene from one hour. At the moment the lead is looking at inspection, they do not know what is happening in packing, and the two hours the lead spends in a meeting are a complete blank.
A walkthrough is a sample, and a manager's eyes open only a few times a day. To change labor allocation on evidence, you need a full count, not a sample: numbers counted all day, at every process, by the same rule.
II. How warehouse labor tracking counts people by process
The TwinTracker UWB anchors fixed around each process receive the signal from the ORBRO Tag each worker wears, and ORBRO Edge RTLS calculates the position. What ORBRO OS2 does on top of that is simple. The manager draws the boundaries of the picking, inspection, packing and shipping zones on the map, and the number of tags inside each boundary becomes that process's current headcount.
Three numbers come out of this.
1. How many people are at each process right now
The current headcount is counted from the tags inside the zone, and how it changed by time of day is kept alongside. The 12 on the plan and the seven in the inspection zone sit on the same screen for the first time.
2. Which aisles people move through
Pick a period and replay the stored location history on the floor layout, and you can see in what order workers moved between processes and which aisles they used most. A stretch that people cross back and forth repeatedly is grounds for changing the work sequence.
3. Where dwell time is longest
Entry and exit times are recorded against the boundaries registered on the map, and the difference between the two times for the same tag is the time spent in that zone. A process where people pile up or dwell time grows becomes a candidate congestion point. Keeping a history of when a zone boundary was crossed is the same principle applied to products in the article on manufacturing process traceability.
One thing needs to be made clear here. A long dwell time does not automatically mean waiting. Someone who stayed a long time in the inspection zone may have been working a long time or waiting a long time. That judgment belongs to the manager who knows the day's workload and the conditions on the floor. Location data narrows down where to look first; it does not say what the problem is.
III. Three records and how they differ
| Item | Shift plan | Floor walkthrough | Location count |
|---|---|---|---|
| What it tells you | Where you decided to put how many people | Where it is crowded at that moment | Where how many people were, all day long |
| Point in time | Before the shift starts | Only the moment you look | The entire shift |
| What remains | A document | A memory | Numbers by zone and by time of day |
| Effort required | Written every day | Walk it every time | Automatic once boundaries are drawn |
The three do not replace one another. The plan is still needed, and the walkthrough sees what numbers cannot show. What the location count adds is the ability to put plan and result side by side in the same unit.
IV. Three ways to turn the numbers back into labor allocation
1. Compare before and after a reallocation
Take the date extra hands were brought in and compare the process records before and after it. In ORBRO OS2, query the headcount by zone for each date, export it to a file, and line up the same process at the same time of day. The day's workload has to be viewed alongside for the comparison to be fair. Put a day with twice the volume next to an ordinary day as they are, and the effect of the reallocation is buried under the effect of the volume.
2. Find the processes short of plan
Set the headcount written in the shift plan against the headcount that actually stayed at that process. Download the zone headcount record and put it next to the roster, and the time slots where 12 were planned but seven were present show up, along with which process they keep repeating at. Break times have to be excluded. Read a slot that is empty because of a scheduled break as a shortage and you have invented a problem that does not exist.
3. Put restricted zones and tag handover into the operating rules
Equipment rooms and storage for high-value goods can be designated as entry-alert zones. When a tag meeting the set conditions enters a registered zone, the operator is notified, and a warning light can be added by connecting an output device. The tags to be issued before a shift and the tags returned after it are checked against the registered device list and their status, but who received which tag, when it was handed over and whether it came back are kept separately in an operations log keyed by tag ID. If tags do not travel with the people, every number above falls apart, so the handover procedure comes before the data.
V. Measure the process, not the person
The day this data starts being used for individual evaluation is the day the project ends. The reason is not ethics but data quality. The moment people learn it is used for evaluation, they leave the tag on the desk and walk, or stage their movements. From then on what is collected is not the real flow but a performed one, numbers that cannot be used as a basis for allocation.
That is why warehouse labor tracking is aggregated from the start by zone, process and time of day. If the screen says "the inspection zone at 3 p.m. is five people short of plan" rather than "who is slow," the conversation turns toward volume and allocation, not toward people. Telling the floor before you start what is measured, why, and what is not looked at is also the fastest way to reduce resistance to adoption. It is not a courtesy; it protects the data.
For the same reason, this article is a different story from clock-in records. How to automate attendance with location data is covered separately in location-based attendance automation. Attendance asks whether someone came in; warehouse labor tracking asks where they were during working hours.
VI. What to decide before you start
- Draw process boundaries in the language of the floor. The names people actually use, picking, inspection, packing, shipping, have to match the physical work areas for the numbers to be readable. For zones that sit next to each other, watch the actual movement and adjust the boundary.
- Match the positioning method to the question. For distribution by process, zone-level accuracy is often enough, so you can start with BLE positioning or smartphone-based mobile positioning; to see movement at the aisle level, a UWB RTLS setup is the right fit. How much precision to buy is decided backwards from what you want to ask.
- Decide the basis of comparison first. Before and after a reallocation, day shift and night shift, peak season and normal: unless you decide what to compare with what, you pile up numbers and change nothing.
- Attach tag handover to the shift procedure. Issue and return have to become one line in the shift meeting, or the data breaks.
- Narrow the first question to one. Start with a single question such as why the afternoon wait at inspection keeps repeating, and within two weeks you have grounds to change the allocation.
In closing
The 12 on the plan and the seven on the floor will keep differing. That is how a logistics center moves. What changes is that the difference no longer vanishes by evening; it becomes the material for the next plan.
ORBRO OS2 is a monitoring and control platform that aligns location, video and sensor data on a single space. Headcount by zone, movement history replay, and entry and exit records are built in, and exported records can be set against the roster or handed to an upstream system. The configuration for warehouse labor tracking with RTLS is laid out on the warehouse worker flow analysis solution page. Tell us which gap at which process you want to see first, and we will start by reviewing a configuration that fits your site.
Recommended Blogs
Forklift Collision Avoidance When AMRs Share the Aisle: Pass UWB Coordinates, Let the Robot Decide
2026-09-16
RTLS Pilot Project: What Your Proof of Concept Should Verify
2026-09-15
Semiconductor Fab Personnel Tracking: Why Location Is Stored Only by Floor and Zone
2026-09-14

A New Era of Logistics: Smart Warehouse Management Powered by GPT-6 and Real-Time Positioning
2026-09-12